Solutions
Custom Color & Functio
Superior

Hardware components often face coating problems such as scratches, corrosion, poor adhesion, uneven coverage, color variation and excessive film buildup. These issues are affected not only by the powder coating itself, but also by substrate material, pretreatment, application conditions and curing parameters.
YATU provides application-oriented powder coating solutions for metal hardware components. We help customers select suitable coating systems based on the actual problem, substrate, environment, appearance requirement and production process.
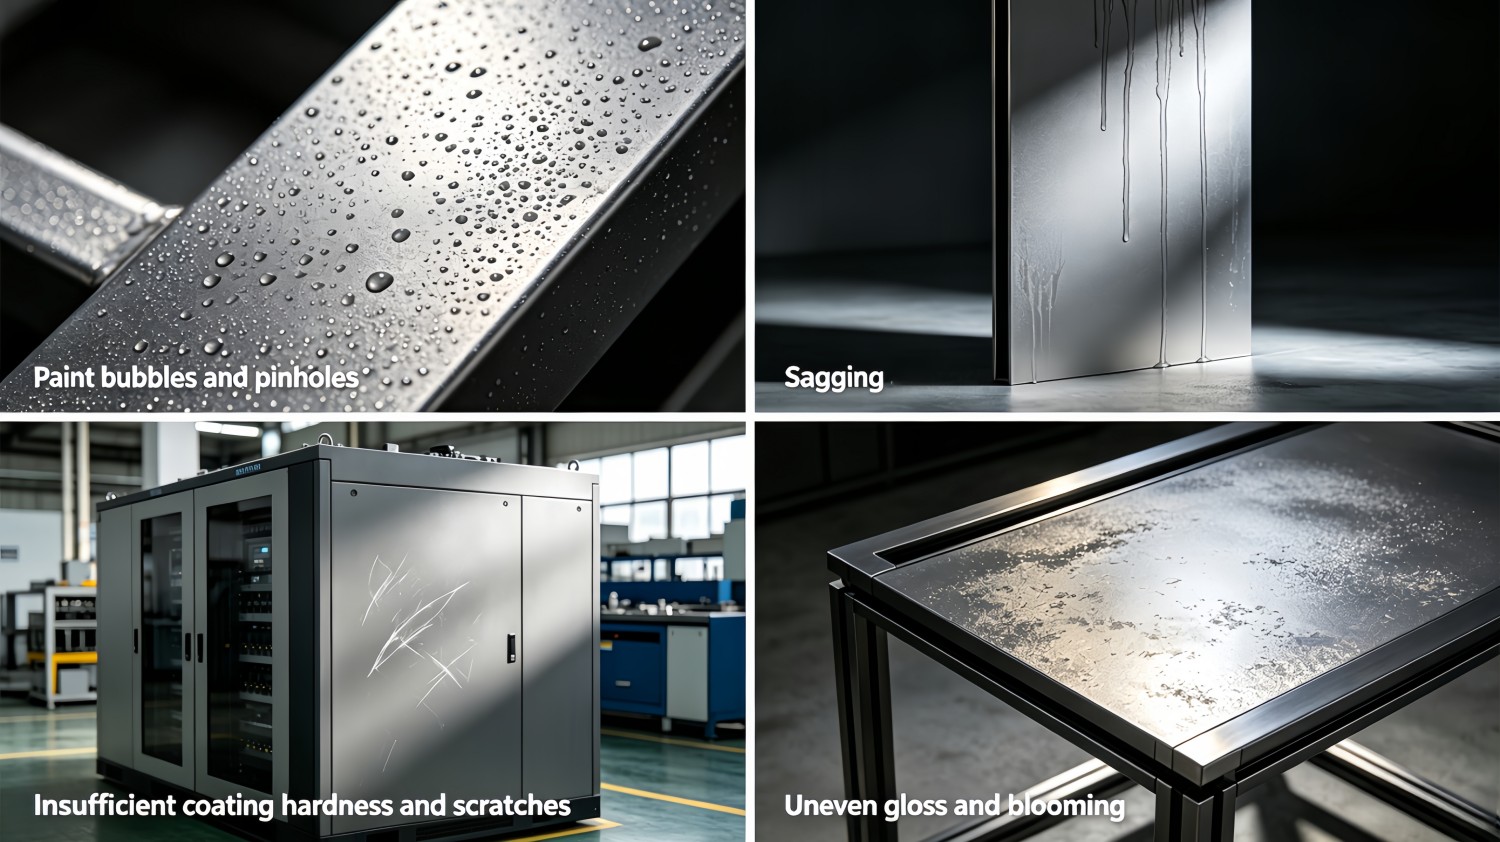
| Common Problem | Possible Cause | Solution Direction |
|---|---|---|
| Scratches or surface wear | Insufficient hardness or unsuitable finish | Improve scratch resistance and select a more suitable surface finish |
| Rust or corrosion | Poor pretreatment, exposed edges or insufficient protection | Improve pretreatment, edge coverage and corrosion resistance |
| Coating peeling | Surface contamination, poor adhesion or incorrect curing | Check pretreatment, adhesion and curing conditions |
| Uneven coating thickness | Inconsistent spraying or grounding | Optimize spray parameters and film-build control |
| Poor edge or recess coverage | Complex geometry or electrostatic shielding | Improve grounding, gun position and application settings |
| Color or gloss variation | Different film thickness, substrates or curing conditions | Use approved samples and tighter process control |
| Excessive coating buildup | Too much powder on functional areas | Control film thickness or mask critical surfaces |
| Surface defects | Poor leveling, contamination or incorrect curing | Review powder flow, substrate condition and curing process |

1. Select according to the scene: Indoor hardware (epoxy polyester blend, high gloss/flat gloss/matte); Outdoor/bathroom hardware (pure polyester weather-resistant, fluorocarbon high-end); High wear-resistant hardware (wear-resistant modified polyester); Decorative hardware (metal bonding powder, high gloss/skin-feel powder).
2. Film thickness standard: 40–60μm for general use, 30–50μm for decorative hardware (thin coating is more efficient and avoids adhesion).
3. Core indicators: Adhesion ≤ Grade 1 (cross-cut test); Scratch resistance (indoor ≥ Grade H, outdoor/bathroom ≥ Grade 2H); Salt spray resistance for bathroom hardware ≥ 1000h, outdoor ≥ 500h; Color difference ΔE < 1.5.

1. Epoxy-polyester blend: The first choice for indoor hardware, with excellent adhesion, good leveling, rich colors, and controllable cost, taking into account both decoration and basic corrosion protection.
2. Pure polyester/fluorocarbon powder: the core choice for outdoor/bathroom use. Pure polyester is water and salt spray resistant, while fluorocarbon is suitable for extremely humid environments, solving the problems of blistering and rusting.
3. Wear-resistant modified polyester: Added wear-resistant filler, hardness reaches 2H level, improves friction resistance, and extends the service life of high-frequency components such as guide rails and hinges.
4. Thin-coat high-efficiency powder: Suitable for small-batch production, reducing powder loss, avoiding stacking and sticking, and improving production efficiency.
1. Pretreatment process: ultrasonic degreasing → pickling/neutralization → phosphating/passivation → drying; Key requirements: no oil stains or oxide layer on the surface to ensure adhesion.
2. Spraying process: A rotating hanger is used for electrostatic thin coating to control the film thickness uniformly and avoid powder buildup and exposed substrate.
3. Curing process: 180–220 ℃ × 10–15min ( low temperature fast curing) to avoid deformation of small parts.
4. Post-processing and inspection: Sorting after cooling to avoid stacking and scratching; mandatory inspection items (cross-cut adhesion, scratch resistance, salt spray, appearance).

YATU supports different appearance requirements, including:
RAL color matching;
customer-supplied color samples;
matte and gloss finishes;
textured surfaces;
metallic effects;
project-specific appearance requirements.
This chapter summarizes the core logic of recommended product combinations for four major application scenarios, facilitating procurement and production implementation. All combinations are adapted to the corresponding scenario's process requirements, balancing cost-effectiveness and quality, and can be flexibly adjusted according to actual project budgets and environmental levels.
1. Core Adaptation Logic: All product combinations follow the principle of "main powder + auxiliary materials + additives". The main powder determines the core performance of weather resistance and corrosion prevention, the auxiliary materials (passivating agent, primer) improve adhesion, and the additives optimize the construction effect and the quality of the finished product.
2. Flexible adjustment principle: In ordinary scenarios, the amount of additives can be reduced to control costs; in high-end scenarios, adhesion promoters and sealants can be added to improve product durability; for mass production, fast-curing and thin-coating formulas should be prioritized to increase production capacity and reduce losses.
3. Color Scheme Recommendations: The recommended color schemes for each scenario are all mainstream and compatible colors in the industry, which can be used directly; custom color schemes (RAL/PANTONE color codes) are also supported, and the color depth and gloss (high gloss/matte/sand texture) can be adjusted according to the decoration style and project needs. For special needs such as metallic effects and wood grain transfer, special auxiliary materials can be used to ensure stable results.
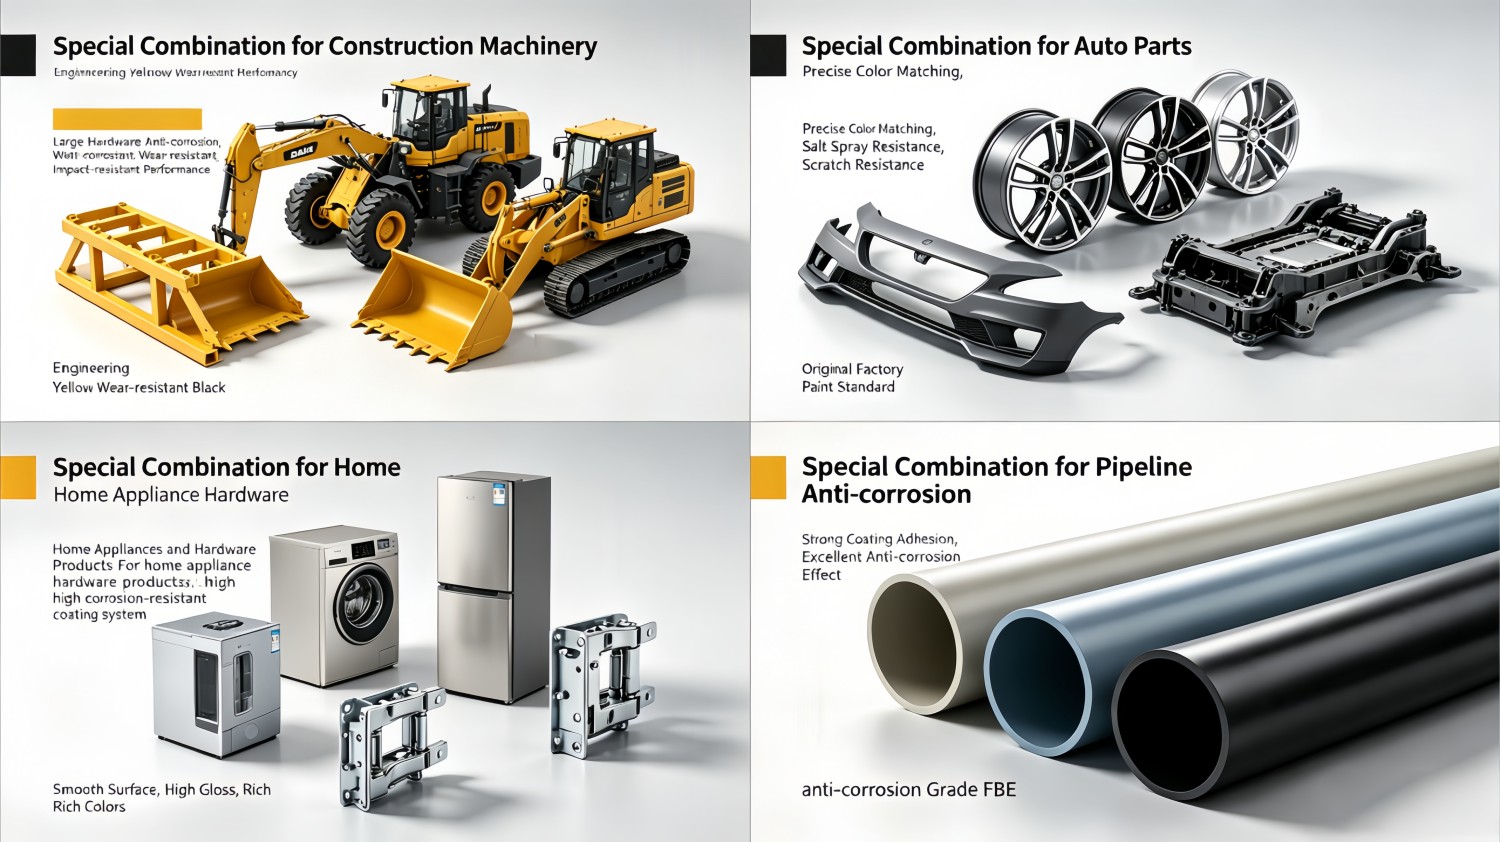
1. Substrate matching: Aluminum profiles/coils → pure polyester/fluorocarbon powder; steel coils/wrought iron → epoxy/epoxy polyester powder; stainless steel → special adhesion-enhancing powder.
2. Environmental priority: Outdoor scenarios prioritize weather resistance (focusing on QUV aging and salt spray testing); indoor scenarios prioritize appearance and basic corrosion protection; coastal/highly corrosive environments use fluorocarbon or ultra-weather-resistant formulations.
3. Process compatibility: Aluminum profiles → conventional electrostatic spraying; coils → high-speed thin-coating and fast-curing spraying; small hardware parts → thin-coating and high-efficiency spraying.
4. Cost balance: Pure polyester powder is selected for mid-range projects (best cost performance); fluorocarbon powder is selected for high-end projects and extreme environments (quality priority); thin-coating and fast-curing formulas are preferred for mass production (cost reduction and efficiency improvement).
Check substrate cleaning, pretreatment, coating adhesion and curing conditions. Peeling is often related to the complete coating process rather than the powder alone.
Corrosion resistance depends on substrate pretreatment, edge coverage, coating thickness and the selected coating system. Required corrosion tests should be defined before production.
Differences may come from film thickness, substrate, curing conditions or process variation. Approved physical samples and controlled production conditions can improve consistency.
Film thickness should be controlled and critical functional areas may require masking. Sample assembly testing is recommended before mass production.

Deeply cultivating the field of metal powder coatings, building a global production and service network, becoming a leading global provider of metal surface coating solutions, and working together with partners for mutual benefit.


